Table of Contents Introduction What smart cold forming actually means
 Skip to content

Key Takeaways
Table of Contents
Sustainability is no longer a marketing slide in the fastener industry. Buyers for automotive, renewable-energy and appliance supply chains now ask for carbon-footprint data, REACH/RoHS declarations and evidence that plants are cutting water discharge and hazardous waste. For cold heading plants, one of the biggest hidden environmental loads sits upstream of the former: wire pre-treatment.
Before wire enters a multi-station cold former, it is usually phosphated and soap-coated so the surface can survive the extreme pressures of deformation. The resulting sludge, spent baths and rinse water can make up a large share of a plant’s hazardous waste and wastewater treatment cost. At the same time, downstream forming precision determines how many of those pre-treatment steps are needed in the first place.
This article explains how two changes—near-net-shape cold forming and polymer-based eco lubricants—work together to cut pre-treatment sludge and material waste. We will look at why the old phosphate-and-soap system is becoming expensive, what green alternatives are now commercially proven, how to maintain tool life during the switch, and how DongRui multi-station formers give plants the precision needed to make the transition pay off.
Wire pre-treatment has historically been treated as an operational detail, not a compliance risk. That is changing because regulators are tightening limits on the substances that leave a typical phosphate line.
EU REACH and RoHS: REACH restricts nickel, chromium(VI) and certain phosphates in manufacturing chemicals; RoHS/ELV keep hazardous substances out of automotive and electronics supply chains. Phosphate baths that contain heavy-metal accelerators require careful chemical management and documented substitution analysis.
Wastewater discharge permits: Limits for total zinc, manganese, phosphate and COD are becoming stricter across Europe, the United States and China. A fastener plant discharging to a municipal system may face surcharges once phosphate or heavy-metal thresholds are crossed.
China GB standards and local emission permits: Provincial limits on wastewater COD, total phosphorus and heavy metals often require physical-chemical treatment plus sludge dewatering. Sludge classified as hazardous waste can cost several times more to dispose of than ordinary industrial waste.
Compliance is no longer a one-time permit. It is a recurring cost made of:
Plants that still rely on conventional phosphate-and-soap lines are finding that a larger share of their operating budget is now spent keeping the pre-treatment bath legal, rather than keeping it effective. This is the pressure that makes alternatives economically attractive.
Phosphating remains popular because it creates a crystalline layer that holds soap lubricant and reduces friction during cold forming. But the process is inherently wasteful.
During zinc or manganese phosphating, metal ions from the bath react with the steel surface and precipitate as phosphate crystals. Some crystals deposit on the wire; the rest fall out of solution as sludge. As bath load increases, the sludge layer at the bottom of the tank thickens, bath chemistry drifts, and coating quality becomes inconsistent. At that point the bath must be dumped, cleaned and rebuilt.
Soap coating adds another waste stream. Excess soap is carried over into rinse stages, increasing COD and foam in wastewater. Soap dust is also a housekeeping and respiratory issue on the shop floor.
| Cost item | Typical annual load for a mid-size fastener plant | What drives it |
|---|---|---|
| Phosphate chemicals | $15,000–$40,000 | Bath volume, replenishment rate, drag-out |
| Sludge removal & disposal | $8,000–$25,000 | Hazardous classification, moisture content, transport distance |
| Wastewater treatment | $10,000–$30,000 | COD, phosphate, zinc/manganese, flow volume |
| Labour & monitoring | $6,000–$12,000 | Bath analysis, permits, operator time |
| Production risk | Variable scrap cost | Bath out of spec → poor coating → die galling |
For a plant running a single phosphate bath, the combined annual cost can easily exceed $50,000 to $100,000, not including the production losses from rework when coating quality drifts.
Beyond direct spend, phosphate lines consume floor space, energy and labour that could be redirected. Removing or downsizing pre-treatment can free up production area near the cold formers, shorten material handling routes and reduce the number of processes a quality manager must supervise.
Green wire preparation is not a future technology. Polymer-coated wire and advanced water-based lubricants are already used by major fastener producers for carbon-steel grades up to about 10.9 and some stainless applications.
In polymer-coated wire, a thin thermoplastic or resin layer is applied to the wire surface at the rod mill or by a specialist wire drawer. The polymer acts as both a corrosion barrier and a solid lubricant film. When the wire enters the cold former, the polymer deforms with the surface, reducing metal-to-metal contact without creating phosphate sludge.
The main advantages are:
Eco lubricants include water-based synthetic fluids, vegetable-oil derivatives and boron-free formulations. They replace or supplement mineral-oil drawing soaps and can be applied as a thin film before the former. Because they contain little or no heavy-metal EP additives, their wastewater load is far lower and their disposal classification is usually simpler.
| Feature | Phosphate + soap | Polymer coating + eco lubricant |
|---|---|---|
| Sludge generation | High | 80–95% lower |
| Rinse water volume | High multi-stage rinses | 60–90% lower |
| Heavy metals in waste | Zinc/manganese/nickel possible | None |
| Disposal classification | Often hazardous | Usually non-hazardous |
| Surface consistency | Bath-dependent | Mill-controlled, uniform |
| Shop-floor cleanliness | Soap dust, wet floors | Dry, low residue |
Polymer coatings work best where surface pressures are moderate and part geometry is not extremely aggressive. The sweet spot includes:
High-reduction, exotic-steel or very large-diameter parts may still need phosphate conversion coatings, but even then a partial switch—using polymer for standard sizes and phosphate only for severe grades—can cut sludge by half.
The most common objection to green lubricants is tool life. If the lubricant film is thinner or less tenacious than phosphate-soap, dies and punches may wear faster or gall. The answer is to match the lubricant to the machine and tooling system, not just to the wire.
Tooling for polymer-coated wire often uses advanced PVD or CVD coatings such as TiAlN, CrN or diamond-like carbon (DLC). These coatings reduce adhesion, dissipate heat and compensate for the lower EP film thickness of polymer lubricants. Reconditioning intervals can actually lengthen compared with uncoated tools running on marginal soap baths.
Green lubricants have less “forgiveness” than thick soap films. Any misalignment, off-centre blow or poor transfer will show up as galling or scoring sooner. This is why a rigid, well-aligned multi-station former is essential when switching away from phosphate. Machines with loose slides, worn cams or weak transfer fingers will make green lubricants look bad even when the lubricant is not the problem.
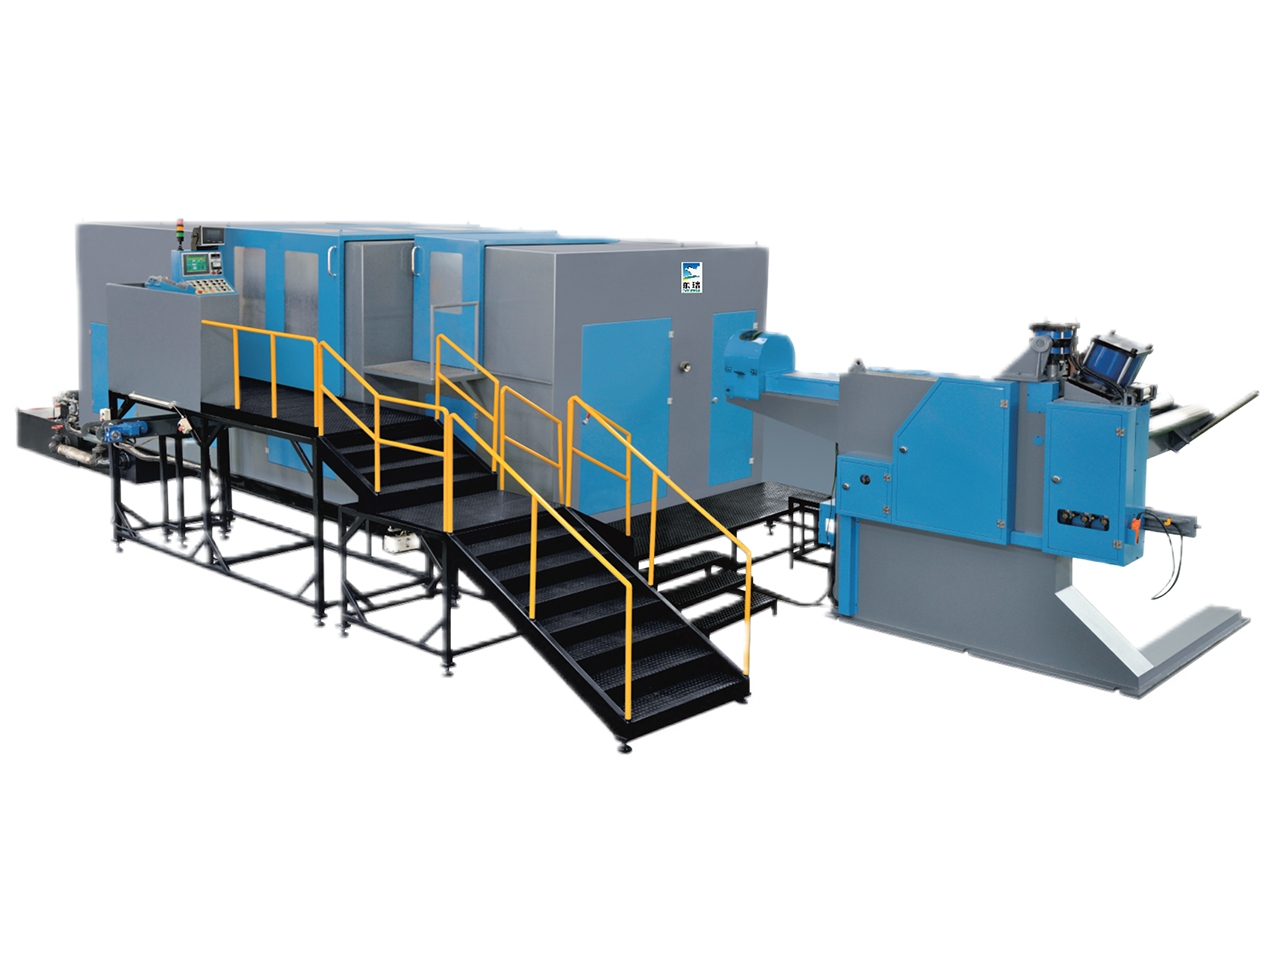
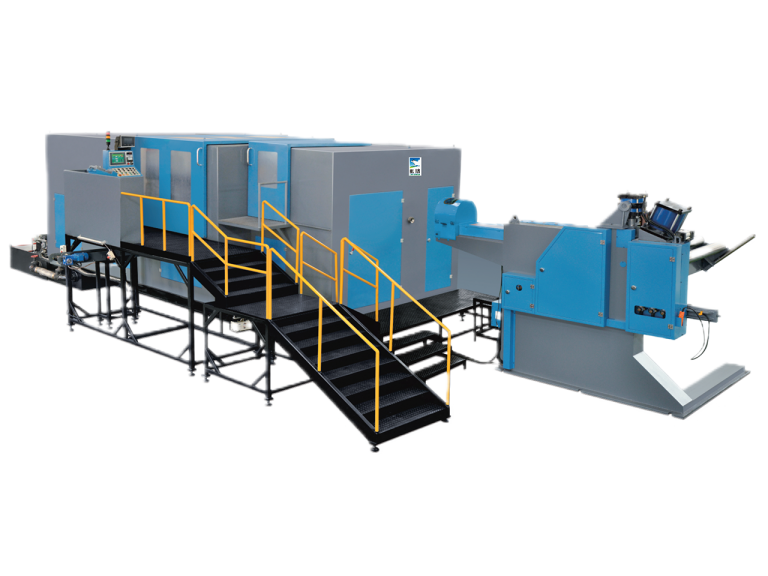
DBP-276S six-station part former delivers the alignment and transfer precision needed for polymer-coated wire and eco lubricants.
Done right, tool life can remain within 5–10% of phosphate-and-soap levels while sludge and wastewater drop by much larger margins.
Green wire preparation reduces the pollution generated per metre of wire. Near-net-shape forming reduces the number of metres of wire that must be pre-treated in the first place.
When a fastener is cold-headed close to final dimensions, there is little or no secondary machining. Every machining operation removed from the routing removes at least one cleaning and handling step, and often removes a separate pre-treatment pass. Wire that goes straight from the drawing line to the former and then to heat treatment avoids intermediate phosphate baths entirely.
Consider a plant producing 10 million medium-carbon bolts per year. If a conventional process routes every bolt through turning after heading, the plant must pre-treat enough wire for the heading stage, then clean and re-coat turned blanks for any secondary forming or heat-treatment step. If near-net-shape forming removes the turning stage, the plant eliminates:
Even if only 30% of the product mix can be converted to net-shape, the wastewater treatment load falls proportionally.
Multi-station formers distribute deformation across several blows. That lowers the reduction ratio in each station, gives the operator more control over material flow, and makes it practical to form heads, shanks, shoulders and extrusions to tight tolerances in a single machine. The result is a part that leaves the former ready for heat treatment or thread rolling with minimal machining.
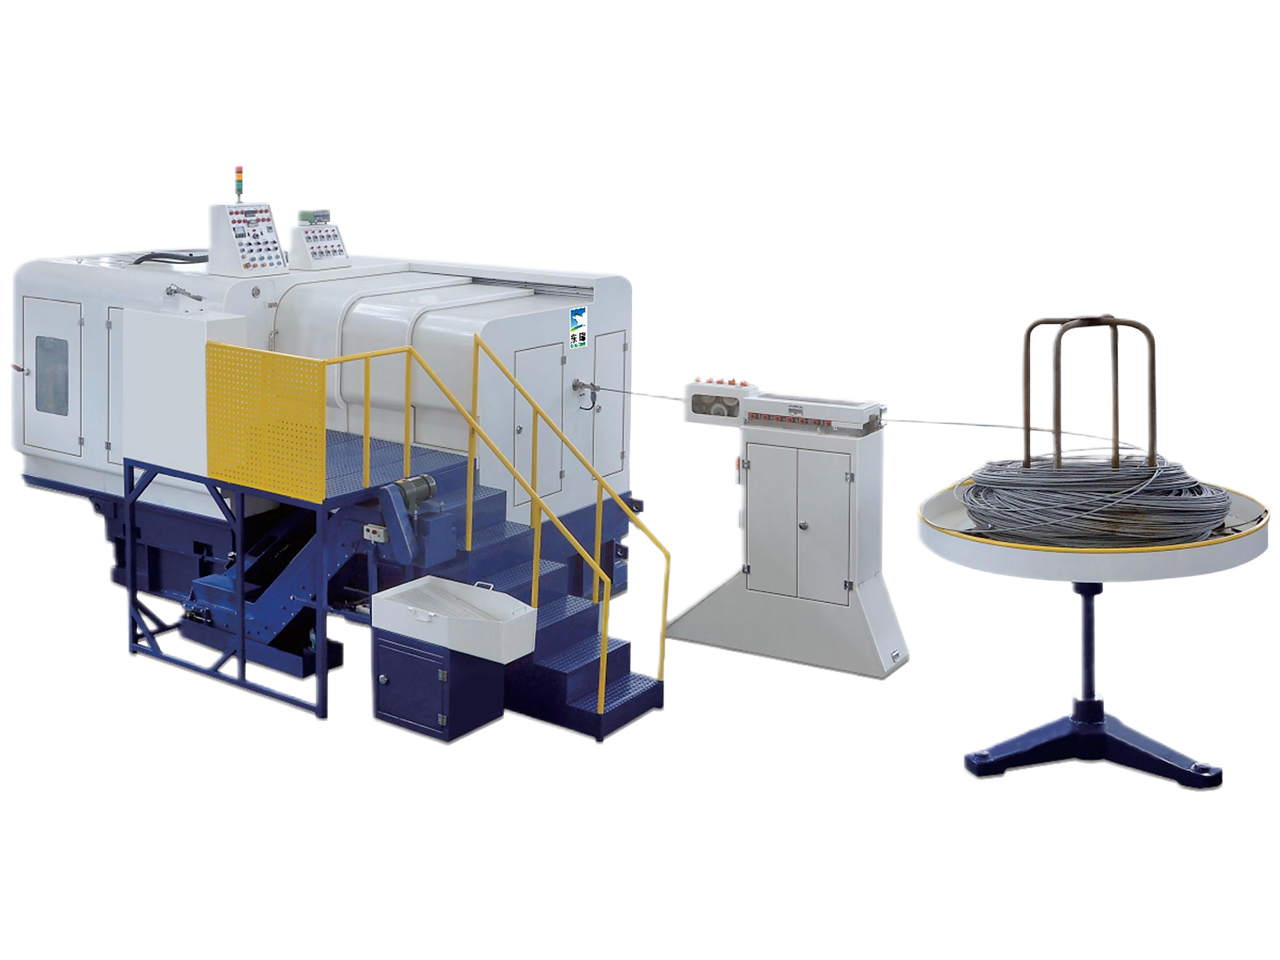
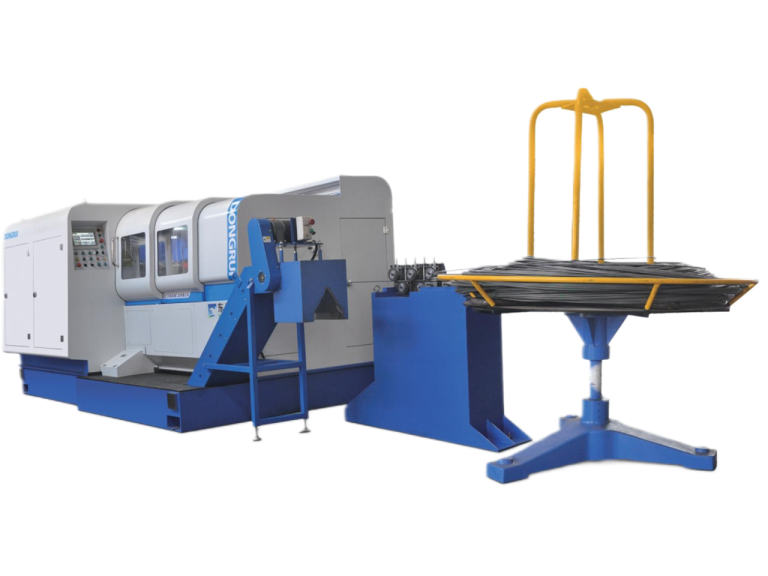
DBP-136LL multi-station cold heading machine forms complex geometries in one pass, reducing downstream machining and pre-treatment demand.
When a plant pairs this capability with polymer-coated wire, the environmental footprint shrinks on both sides of the process: less sludge from wire preparation, and fewer pre-treatment cycles because the part is already near final shape.
Switching from a phosphate line to a green process is not as simple as ordering polymer-coated wire. A staged approach protects production while the plant learns the new system.
Measure baseline data before any change:
This baseline becomes the benchmark for ROI and compliance reporting.
Choose one product family with moderate reduction ratios and stable volumes. Run polymer-coated wire on a single cold former with PVD-coated tooling for at least four production shifts. Record surface finish, dimensional drift, tool polishing interval and scrap rate.
Ramp up only after the trial proves equivalent part quality and acceptable tool life. Move to the next easiest product family while keeping phosphate available for severe grades. Over 12–18 months, most standard carbon-steel fasteners can usually be converted.
As green lubricants replace forgiving soap films, machine rigidity and transfer precision become the limiting factors. If existing formers cannot hold the tolerances needed, upgrading to a modern multi-station machine becomes part of the sustainability investment. The payback comes from lower pre-treatment operating cost, reduced scrap, and the ability to quote into environmentally screened supply chains.
Sustainable cold heading is not only about energy labels or recycled packaging. The largest environmental opportunity in many fastener plants is hidden in the phosphate-and-soap line that prepares wire for forming. By replacing or reducing that pre-treatment with polymer-coated wire and eco lubricants, plants can cut sludge by 80–95%, lower wastewater treatment costs, and simplify compliance.
The economics improve further when the switch is paired with near-net-shape cold forming. Fewer machining operations mean fewer pre-treatment cycles, less wire handling and lower scrap. Modern multi-station cold formers provide the precision and tooling compatibility to make green wire preparation reliable at production speed.
DongRui multi-station formers are designed with the rigidity, die alignment and transfer accuracy that green lubricants demand. If your plant is reviewing its environmental footprint or facing tighter wastewater permits, upgrading both the wire preparation process and the forming machine together delivers the strongest ROI.
Explore DongRui Multi-Station Cold Formers
Polymer-coated wire typically stores for 6–12 months in a dry environment. Humidity is the main risk: a damp storage area can cause the coating to blister or stick, leading to feeding problems in the former. Keep coils under cover, avoid ground moisture, and follow the supplier’s recommended first-in-first-out rotation. If storage conditions are poor, expect shorter effective shelf life and occasional recoiling issues.
Compatibility depends on die alignment, surface pressure and tooling coatings, not just the machine brand. Modern multi-station formers with rigid beds, precise transfer and PVD-coated dies usually run polymer-coated wire well. Older or loose machines may experience galling because the thinner polymer film cannot compensate for misalignment. A short trial on your specific former geometry is the safest way to confirm compatibility before a full rollout.
The relevant rules depend on your market and discharge route. In Europe, REACH governs the chemicals used and may restrict nickel, chromium(VI) and certain phosphates. RoHS/ELV limits hazardous substances in automotive and electronics fasteners. In the United States, local wastewater permits set discharge limits for zinc, manganese, phosphate and COD. In China, GB wastewater standards and provincial permits control total phosphorus, heavy metals and COD. A green process should be documented with supplier declarations, test reports and internal audit records to satisfy customer and regulator questionnaires.
Table of Contents Introduction What smart cold forming actually means
Reading time: ~9 min | Categories: Cold Forging Technology, Industrial
Wind turbines need large, fatigue-resistant bolts. See why 8-station+ high-tonnage
1. Introduction A finished bolt sitting in a bin looks
 Optimized by Seraphinite Accelerator