Table of Contents Introduction What property classes mean The quench
 Skip to content

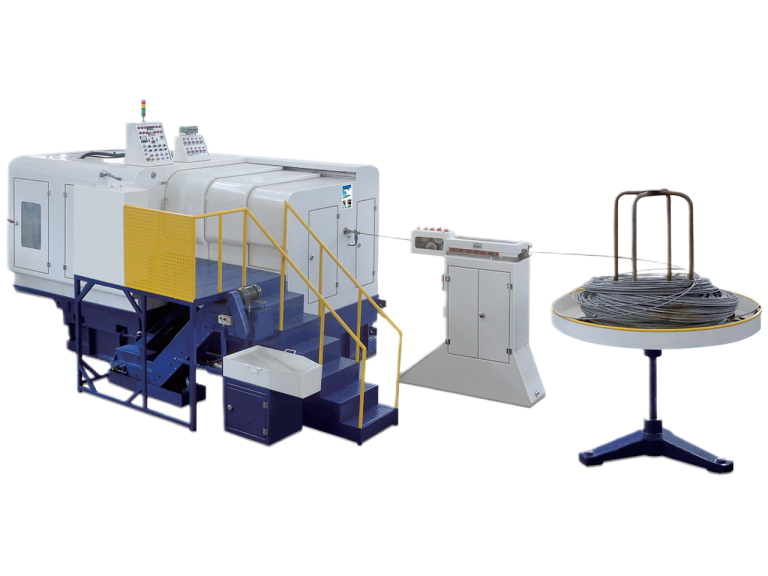
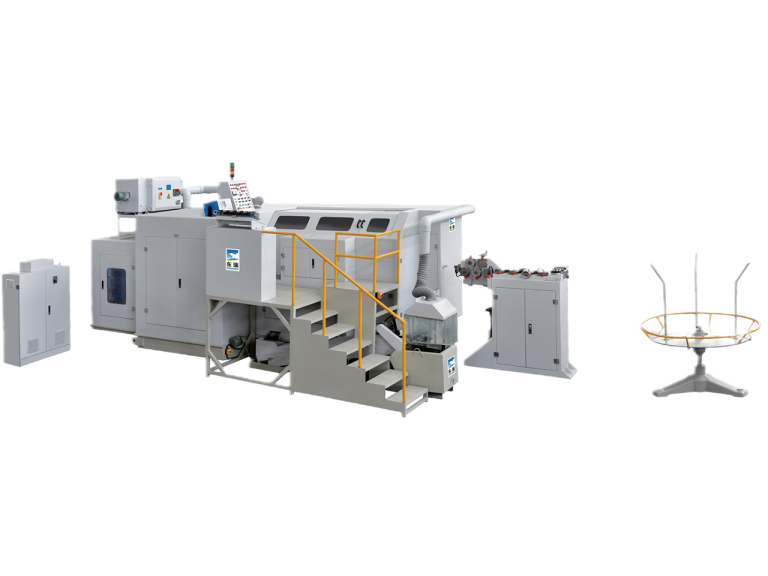
Scrap is the quiet margin killer in fastener manufacturing. A plant running a M10 bolt on a CNC lathe can lose 50–60% of its purchased wire as chips, and even on a well-tuned cold forming line, off-cut ends, flash, trim, rejected heads, and reworked blanks quietly reduce the yield that the whole business plan depends on. For years this loss was treated as an unavoidable cost of doing business. In a market where steel prices move, energy costs rise, and end customers demand lower part prices every quarter, it is no longer acceptable.
Near-net shape cold forming changes the economics. By moving material to where it belongs instead of cutting it away, multi-station formers produce a blank that is within a millimetre or two of the finished fastener, typically with material yield above 90% and often above 95% for simpler geometries. This article explains how gram-level scrap differences compound into six-figure annual savings, why the same process reduces energy use and helps meet green manufacturing requirements, and how to audit your own scrap rate and upgrade profitably.
Table of Contents
Key Takeaways
Fastener plants rarely lose money on one big item. They lose it in small, persistent streams: the off-cut tail from each cut-off, flash trimmed from the head, short blanks rejected at in-process inspection, title-bar ends that never get scheduled, and swarf collected from the machines at the end of the week. Individually each looks trivial. Together they define the plant’s true material yield.
Three external pressures have turned that yield gap into a strategic issue:
| Waste stream | Where it appears | Typical share of input material | Recoverable? |
|---|---|---|---|
| Off-cut / tail | Cut-off station each cycle | 2–6% | Partly — shorter tailor-made cut lengths |
| Flash & trim | Head trimming, flash removal | 1–5% | Yes — better die fit and closure |
| Rejected blanks | In-process inspection, first-piece check | 0.5–3% | Yes — process stabilisation, sensors |
| Swarf / chips | Secondary machining, thread cutting | 20–60% on turning routes | Only by re-melting (loss of energy) |
| Scale / oxides | Hot forging routes | 1–3% | Partly — descaling control |
The important distinction is that flow scrap (off-cuts, trim, rejections) stays inside the plant and can be reduced by process control, while removal scrap (chips from turning) leaves the plant as swarf and has already consumed energy to become that way. Cold forming attacks both, which is why it is such a powerful margin tool.
Cold forming is a mass-conserving process. A wire rod of known diameter and length is cut to a blank, then upset, gathered, extruded, and shaped station by station until the blank carries the full volume of the finished part. The only material that leaves the machine is flash from the die split line and the cut-off tail — a tiny fraction of the original rod.
Turning is the opposite: it begins with a bar far larger than the finished part and removes material until the shape appears. Every chip represents steel that was mined, rolled into rod, paid for, and then discarded — along with the energy it took to machine it away.
| Process | Material route | Typical yield | Secondary operations | Energy profile |
|---|---|---|---|---|
| CNC turning from bar | Removal (subtractive) | 40–60% | Thread cutting, facing, drilling | High — cutting power + chip handling |
| Hot forging + machining | Deformation then removal | 65–80% | Descaling, machining, grinding | Medium-high — reheat, scale loss |
| Cold forming (multi-station) | Deformation only | 90–98% | Thread rolling only (usually) | Low — no cutting, no reheat |
| Cold forming + minimal finish | Deformation only | >95% | Thread rolling, heat treatment | Lowest |
This comparison is explained in more depth in our article on how multi-station formers reduce raw material waste, and the process-selection logic against hot forging is covered in cold forging vs. hot forging vs. machining. What matters here is the number: each percentage point of yield is worth real money on every shift, every week, all year.
Your choice of machine determines whether you can actually capture that yield. Station count, die accuracy, and transfer precision decide how close to net shape you can get without cracking or flashing. Our guide to multi-station cold former configurations is a good starting point if you are still comparing station counts.
Scrap reduction is easy to dismiss because the numbers look small per piece. They are not. Fastener plants run millions of pieces per year, and material cost scales linearly with volume.
Worked example — an M10×50 socket head cap screw in class 12.9, forged blank mass ≈ 39 g, rod price ≈ 900 USD/tonne:
| Scenario | Scrap per piece | Pieces / year | Scrap mass / year | Material value lost / year |
|---|---|---|---|---|
| Turned from bar (55% yield) | 32 g | 20,000,000 | 640 t | ≈ 576,000 USD |
| Cold formed, 94% yield | 2.3 g | 20,000,000 | 46 t | ≈ 41,000 USD |
| Cold formed, 97% yield | 1.2 g | 20,000,000 | 24 t | ≈ 21,000 USD |
Closing the gap between a 94% and a 97% line is worth around 20,000 USD per year in material alone on a single part number — before counting the avoided machining, chip disposal, labour, and energy. Add a second and third part number on the same machine and the annual saving scales quickly into six figures. That is why gram-level tuning is worth a maintenance engineer’s attention.
The lever that gets you from 94% to 97% is precision, not optimism:
Defects that destroy yield in the first place are covered separately: our piece on eliminating necking and cracking in cold heading details how reduction ratio and die clearance control scrap at the source.
Circular economy is not only about material yield. It is about using less input for the same output — and cold forming is structurally more resource-efficient than the alternatives.
Cold forming happens at room temperature. There is no reheating, no oxidation scale to remove, and no cutting fluid flood required to evacuate chips. The energy per part is concentrated in the drive and the wire drawing upstream, where it must be anyway. Turning the same part spends extra energy creating chips, moving chips, and disposing of them.
| Resource | Turning route | Cold forming route | Why |
|---|---|---|---|
| Electricity per part | High (cutting + pumps + chip conveyor) | Low (drive and lubricant supply only) | Deformation replaces cutting |
| Water & cutting fluid | High volume, needs treatment | Minimal, mostly lubrication | No chip evacuation requirement |
| Scale / oxides | None (but bar must be clean) | None | No heating cycle |
| Swarf to re-melt | Large volumes, high re-melt energy | Near zero | Material stays in the part |
| Part life expectancy | Lower (severed grain flow) | Higher (continuous grain flow) | Fewer replacements over service life |
There is also an indirect circular benefit that is easy to miss. Because cold forming preserves continuous grain flow, cold-formed fasteners generally deliver higher fatigue life than turned equivalents. A bolt that survives longer means fewer replacements in service, less material consumed across the product’s lifetime, and a smaller end-of-life footprint. For OEMs reporting Scope 3 emissions, that downstream saving is increasingly part of the conversation.
Plants that can evidence material efficiency with per-part yield data are better positioned for green procurement requirements, ESG questionnaires, and preference in markets with circular-economy regulation. The data is easy to generate if the plant already tracks production counts — which makes the reporting work a by-product of ordinary shop-floor discipline.
Achieving near-net shape is not just about the machine’s tonnage. It is about holding dimensional accuracy station after station, shift after shift, so that the blank needs nothing except threading. That is where DongRui formers are configured.
DongRui multi-station formers are built to remove secondary operations from the process chain:
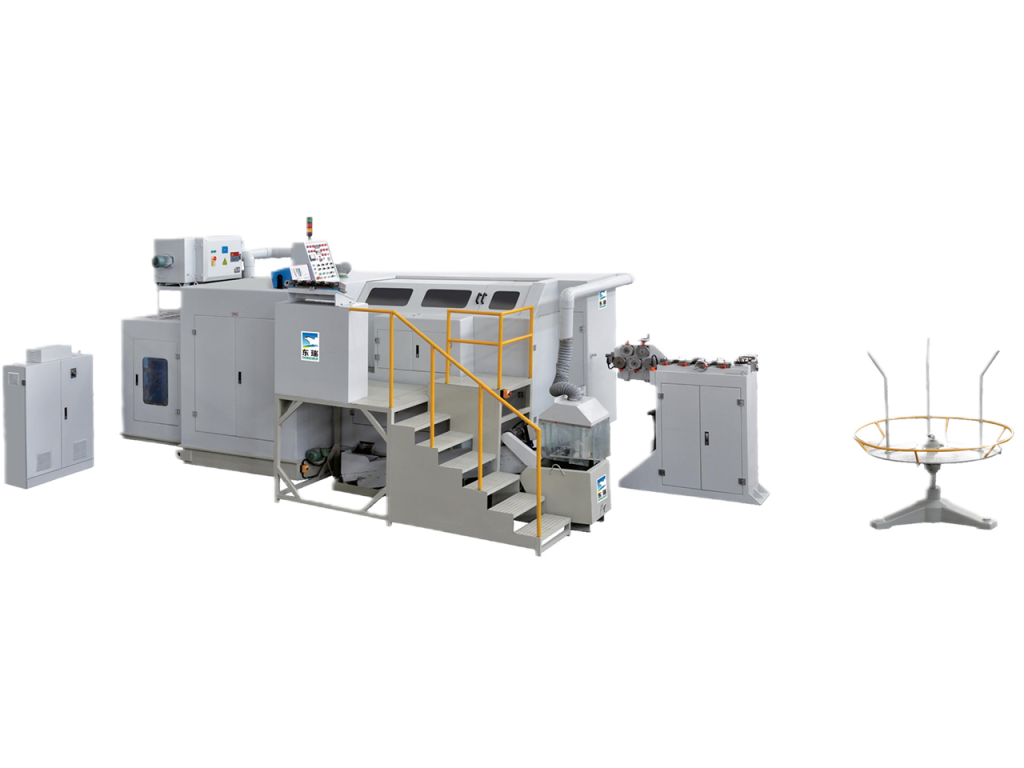
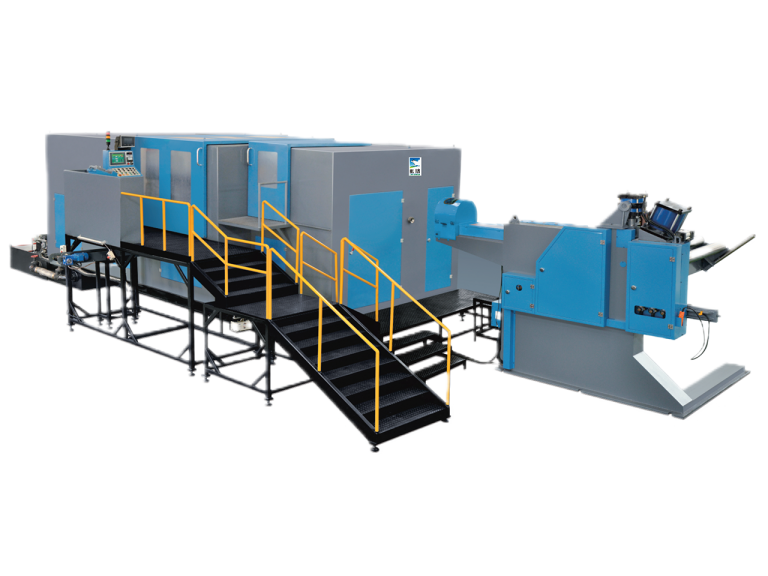
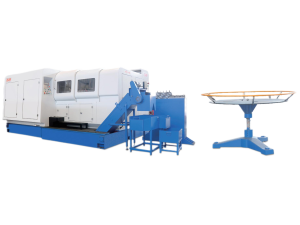
DongRui DBP-276S six-station part former — station-by-station deformation that takes a blank to near-net shape, minimising flash and trim scrap.
The DBP-276S six-station part former is a typical example: six stations give the process enough steps to gather, upset, extrude, and shape a fastener blank to a tolerance that most customers accept without secondary machining. For smaller diameters where cycle rate matters more than part size, the DBP-136LL multi-station cold heading machine delivers the same principle at higher output.
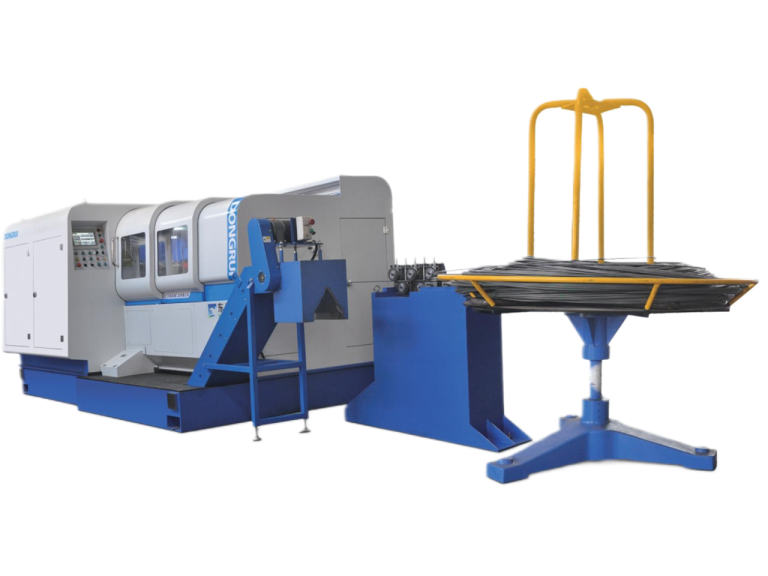
DongRui DBP-255SL high-precision intelligent cold heading machine — consistent blank length and stable forming load for high material yield.
Most plants have never calculated their true material yield. They know the total scrap rate, which includes machining scrap, but they cannot separate the streams that are actually controllable. A four-step audit fixes that and produces the numbers finance will accept.
Weigh incoming rod against the mass of good parts shipped over a representative period, plus all known in-plant returns. The difference is your real yield loss. Express it as a percentage of input mass, not as a percentage of pieces, so it can be compared across part numbers.
Classify losses as: off-cut/tail, flash and trim, in-process rejects, title-bar ends, and secondary machining swarf. Each stream gets a mass and a value. This is the step that makes the improvement plan obvious — most plants find that one stream dominates.
For each significant part, calculate the gain from a target yield (for example 94% → 97%) using current rod price and annual volume. Include the avoided machining time and disposal costs, not only material. This converts a shop-floor observation into a business case.
Run the improvement on one machine and one part number for a defined window. Log per-station forming load, blank length distribution, rejection cause, and die life. If the pilot holds, extend it; if it drifts, the monitoring data tells you which station needs attention.
| Audit step | Output | Typical finding | Next action |
|---|---|---|---|
| True yield measurement | % of input lost | Often 5–15% hidden outside reported scrap | Set a baseline and target per part |
| Stream separation | Mass + value per stream | One stream usually dominates | Focus improvement on that stream |
| Financial model | Annual USD saving | Usually 3–5× the obvious material loss | Present to finance; approve tooling budget |
| Pilot run | Verified yield + drift data | Yield holds for weeks, not hours | Roll out to the rest of the line |
When the finding points toward a process change rather than a tuning change, the decision is a machine decision. Screening the right platform is a matter of matching station count, tonnage, and rigidity to the part family — a step we walk through in matching production speed to your fastener demand, with cost mechanics covered in how cold heading machines cut production costs.
Scrap reduction is no longer an environmental nicety for fastener plants. It is one of the few levers that simultaneously lowers cost per piece, improves energy efficiency, and strengthens the plant’s position in green supply chains. Near-net shape cold forming delivers all three, because it keeps material in the part instead of throwing it away.
The economics are unusually forgiving. A fraction of a gram per piece, repeated across millions of pieces, becomes a six-figure annual difference. The plants that capture it are the ones that measure true yield, separate their waste streams, and treat precision as a margin function rather than a quality function.
DongRui multi-station formers are configured for exactly this objective: station layouts that reach net shape, rigid frames that keep die alignment under load, and monitoring options that protect yield shift after shift. From the six-station DBP-276S to high-precision intelligent models, the machines are built to remove secondary machining from the process — which is where the scrap, the cost, and the carbon all disappear together.
Explore the DongRui DBP-276S Six-Station Former
Related reading:
Most commercial fastener grades work well: low-carbon steels (Sae 1008/1010/1012), medium-carbon (Sae 1035/1045), boron steels (Sae 10B18/10B21/10B22 for class 8.8–12.9), alloy steels (Sae 4140, 4340), stainless grades where ductility allows (304, 316, and 420/430 for certain geometries), and non-ferrous materials such as aluminium alloys and copper alloys for softer parts. Formability depends mainly on elongation and reduction of area at room temperature: higher ductility permits more deformation per station and larger upset ratios. Materials with low inclusion content and consistent wire diameter form most reliably and scrap least. Our article on cold heading titanium and high-temperature alloys explains how to handle difficult alloys that sit at the edge of formability.
Yes, but the value depends heavily on the stream. Clean title-bar ends, off-cuts, and rejected blanks can be baled and returned to the steel mill — often at 60–90% of raw material value, which makes them effectively free revenue rather than waste. Swarf from cutting operations is contaminated with cutting fluid and typically returns much less per tonne, and it represents energy that has already been spent. The best strategy is therefore to prevent the scrap rather than recover it: lowering the waste stream raises the plant’s yield more than any downstream recycling programme. Flash and trim from cold forming are usually clean and easy to bale, which is another quiet advantage over machining routes.
Tooling is the main incremental cost of moving closer to net shape, because tighter clearances and better die materials cost more and need more disciplined maintenance. In practice the offset works in three ways. First, higher yield pays the tooling back directly — on a mid-size part number, material savings alone often cover the premium within one to two years. Second, less flash means less trimming and less rework, reducing labour per good part. Third, longer die life from stable alignment lowers the cost per piece over the die’s total output. Carrying these as cost-per-1000-pieces figures — rather than absolute tooling price — is how the business case should be presented. We cover die materials, coatings, and reconditioning intervals in our cold heading die design and maintenance guide.
Table of Contents Introduction What property classes mean The quench
Table of Contents Introduction Daily Inspection Checklist Weekly and Monthly
Table of Contents Introduction Why NEV is the fastest-growing market
1. Introduction If you’re in the market for a multi-station
 Optimized by Seraphinite Accelerator