1. Introduction A single M6 engine bolt may look identical
 Skip to content

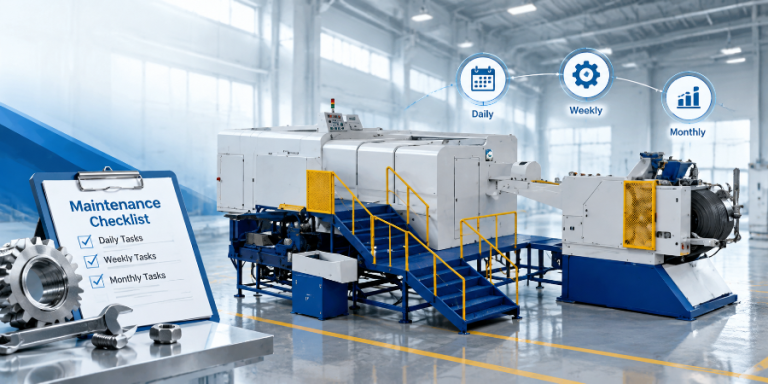

This page is a printable, tick-box maintenance checklist for cold heading machines — built to live at the operator station, not on a screen. For the why behind each task and the workflow for diagnosing failures, pair it with our full guide: Cold Heading Machine Maintenance & Troubleshooting: A Practical Guide to Reducing Downtime and Extending Tool Life. Use this checklist on the floor every shift; open the guide when something actually breaks.
☐Print one copy per machine and keep it at the operator station.
☐Assign an owner for each frequency: shift lead = daily, maintenance tech = weekly / monthly / quarterly.
☐Tick every box as you go — a blank box means the task was not done.
☐Review the sheet weekly against the shift downtime log; flag repeat faults upward.
☐Lubricate slides, ways and transfer rails; confirm the oil reservoir level.
☐Clear swarf from the cut-off and ejector areas — the task that prevents most sudden stops.
☐Listen for abnormal noise or vibration at each station during the first run of the shift.
☐Verify wire feed: straightener and wire rolls seated, no slack, correct coil on the stand.
☐Visual check for hydraulic / pneumatic leaks; top up only after LOTO (see Safety).
☐Confirm all guards closed and the area clear before restarting after any stop.
☐Verify die alignment and transfer timing across all stations.
☐Check belt, chain and feed tension — a slack drive shifts the stroke relationship.
☐Inspect punch and die for early wear or chipping; sample cut-off length for consistency.
☐Tighten loose fasteners on moving parts before drift becomes a short part.
☐Measure die wear against the qualified limit; do not run past it.
☐Inspect dies and punches for cracks with MPI or dye penetrant before failure.
☐Replace tooling on the schedule, not on the breakdown — a failed die can damage the punch and holder.
☐Stock-take the wear parts that fail most often so a planned change never waits on a supplier.
☐Review the downtime log; escalate any fault that repeats two weeks running.
☐Calibrate transfer timing and the stroke relationship between stations.
☐Inspect the transmission — crank, cam and gears — for wear before it fails loudly.
☐Check foundation bolts and overall machine alignment.
☐Flush the lubrication system where the design allows it.
The principles are the same; the emphasis shifts with how fast strokes accumulate. The DBHP-6 high-speed cold former (up to 450 pcs/min for M6) and the DBHP-8 (350 pcs/min for M8) pack strokes faster than a slower line, so lubrication and feed checks matter more, not less — short, frequent planned stops keep the rate instead of one long stop after a failure. The DBP-136L and DBP-206L multi-station part formers carry more stations, which means more alignment points and more places for transfer timing to slip; add per-station die-wear checks and a tighter transfer-timing review, because a fault at station three shows up as a short part at station six. The DBF-134L (8–12 mm standard work) runs the standard list. High speed rewards discipline because it punishes neglect quickly.
Before any check that opens a guard or touches a moving part, isolate power and apply Lock-Out / Tag-Out; verify zero energy. A header runs at high force, and a released component can injure without warning. Keep routine checks inside the guard-closed scope and send structural repairs to trained service — OEM spares are matched to the load and tolerance, and the fitment guidance is part of the value.
☐Repeated part shorts after an alignment check — possible transfer fault, not a die issue.
☐Cracked die or punch — stop the run; a cracked tool can take the holder with it.
☐Overload trips or jams from an oversize blank or a foreign object (hard inclusion) in the wire.
☐Alignment drift ignored for weeks, now pushing a punch into a mis-seated die.
None of these is mysterious after the fact — the structured root-cause workflow for each lives in our guide: Cold Heading Machine Maintenance & Troubleshooting: A Practical Guide to Reducing Downtime and Extending Tool Life. Keep routine checks in house; route structural and high-load work to trained service.
The machine is kept by the cadence, not by the repair. Print this checklist, staff it as a fixed task rather than a reaction, and keep the common wear parts in stock. For the full troubleshooting workflow, tool-life tracking and the machine-design factors behind a low maintenance load, read our complete guide: Cold Heading Machine Maintenance & Troubleshooting: A Practical Guide to Reducing Downtime and Extending Tool Life. Zhejiang Dongrui supplies the DBHP-6 / DBHP-8 high-speed formers, the DBF-134L for 8–12 mm work, and the DBP-136L / DBP-206L multi-station part formers — contact us for matched spares and a service schedule for your model, and turn maintenance from a cost into the reason the line stays running.
1. Introduction A single M6 engine bolt may look identical
Table of Contents Introduction Daily Inspection Checklist Weekly and Monthly

Table of Contents Introduction What Is a Multi-Station Cold Former
Table of Contents Introduction What Defines Standard vs Non-Standard Bolts
 Optimized by Seraphinite Accelerator