Reading time: ~8 min | Categories: Cold Forging Technology, Equipment
 Skip to content

Aluminum fasteners used to be the exception. Today they are becoming a requirement in weight-sensitive applications, from EV battery trays and inverter housings to consumer electronics enclosures and lightweight automotive assemblies. Aluminum offers roughly one-third the density of steel, good corrosion resistance, and excellent electrical and thermal conductivity. The challenge is forming it reliably at speed in a cold heading process that was originally developed for steel.
This guide explains why lightweighting is driving demand for aluminum cold heading, what makes aluminum wire difficult to form, and how die geometry, coatings, lubrication, and machine control turn those difficulties into a stable production process. It is written for fastener buyers, plant engineers, and quality managers who are considering aluminum as a standard material rather than a special job.
Table of Contents
Key Takeaways
Steel remains the default fastener material for heavy-duty structural joints, but designers increasingly specify aluminum wherever mass reduction matters. The most visible drivers are:
These applications share a common manufacturing constraint: they need millions of small, consistent fasteners, often with tight head profiles and clean surfaces. That is exactly what cold heading does well. The question is no longer whether aluminum can be cold headed, but how to set up the process so it competes with steel on cost and consistency.
| Market | Typical aluminum fastener | Key property | Why cold heading fits |
|---|---|---|---|
| EV battery trays | M5–M8 screws, busbar bolts | Lightweight, non-magnetic | High volume, tight tolerances |
| Automotive body | Trim screws, structural bolts | Low mass, corrosion resistance | Net-shape forming reduces machining |
| Consumer electronics | M1.2–M3 micro screws | Non-magnetic, clean finish | Small parts at very high speed |
| Marine / HVAC | Self-tapping screws, rivet bolts | Corrosion resistance | Less secondary finishing |
Aluminum behaves differently from steel in a cold heading die, and the differences matter from the first station.
Aluminum has a lower elastic modulus than steel, so it deforms more easily under load. But it also springs back more when the punch retracts. The result is a part that may look formed in the die but opens slightly after ejection, affecting head height, shank diameter, and concentricity. Holding tight tolerances requires over-forming slightly and using final calibration stations.
Aluminum is soft and tends to weld or gall against tool steel under pressure, especially when sliding contact occurs during extrusion or upsetting. Once aluminum starts to build up on the punch or die surface, it drags material on subsequent parts, producing scoring, dimensional drift, and surface defects. This is the single most common reason aluminum cold heading lines fail to reach stable cycle rates.
Although aluminum is softer than steel initially, it work-hardens quickly. A part that needs a large head or deep extrusion may exceed the material’s formability if the deformation is concentrated in too few stations. Multi-station formers spread the work and keep each step within the safe forming window.
| Behavior | Steel (typical) | Aluminum (typical) | Process implication |
|---|---|---|---|
| Elastic modulus | ≈ 210 GPa | ≈ 70 GPa | More springback; calibration needed |
| Yield strength | Variable; often higher | Lower, then work-hardens | Lower initial force, but watch station limits |
| Galling tendency | Low | High against uncoated steel | Coatings and lubrication essential |
| Thermal conductivity | ≈ 50 W/m·K | ≈ 200 W/m·K | Heat escapes quickly; less thermal distortion |
| Density | 7.85 g/cm³ | 2.70 g/cm³ | 65% mass reduction; lower shipping and handling cost |
The same multi-station approach that helps difficult steel alloys also helps aluminum. Our article on multi-station cold former configurations explains why spreading deformation across stations improves formability for any material.
Tooling is where aluminum cold heading is won or lost. The goal is to let the material flow without sticking, galling, or tearing. Three tooling decisions dominate the outcome.
Aluminum flows more freely than steel, but it is also less forgiving of sharp corners. Dies designed for aluminum use slightly more open entry angles and larger corner radii than steel dies. This reduces the tendency for the wire to fold, buckle, or tear at the head-to-shank fillet, and it lowers the pressure required for the same deformation.
A polished die surface reduces adhesion. Beyond polish, physical vapor deposition (PVD) coatings such as TiN, TiAlN, and CrN, or diamond-like carbon (DLC), create a hard, low-friction barrier that aluminum does not weld to. Coated tools typically last several times longer than bare tool steel in aluminum and produce a cleaner part surface.
For prototyping and low volumes, high-quality tool steel with a good coating may suffice. For high-volume aluminum runs, tungsten carbide or ceramic inserts are often justified because they resist both wear and galling under continuous contact with soft aluminum. We discuss die materials and reconditioning intervals in more detail in our guide to cold heading die design and maintenance.
| Tooling choice | Effect on aluminum forming | When to use |
|---|---|---|
| Polished tool steel | Reduces adhesion, low cost | Low-volume trials and short runs |
| PVD-coated dies | Hard barrier, lower friction, longer life | Production runs of 100k+ parts |
| Tungsten carbide inserts | Excellent wear and galling resistance | High-volume, tight-tolerance parts |
| Open entry angles + radii | Lower forming pressure, fewer folds | Always, but especially large heads |
Sticking and scoring usually appear together. A small amount of aluminum transfers to the die, the next part drags against that buildup, the surface scratches, and the scratches become nucleation sites for more buildup. Breaking the cycle requires clean lubrication, controlled speed, and active monitoring.
Aluminum forms best with lubricants that maintain a stable film under pressure without reacting with the surface. Wax-based, oil-based, or synthetic formulations with extreme-pressure additives are common. The lubricant must be applied evenly to the wire before it enters the cut-off and must remain intact through each station. Dry or patchy lubrication is the leading cause of scoring.
High-speed forming generates heat at the die-wire interface. Aluminum conducts heat well, which helps, but if the local temperature rises enough to soften the lubricant film, adhesion begins. Slowing the stroke slightly, improving die cooling, or adding dwell time at peak load can extend stable run time between tool cleanings.
Load monitoring catches the drift before it becomes visible scrap. As aluminum builds up on a punch or die, forming force changes. A well-tuned sensor system flags the trend and stops the machine before a batch of scored parts is produced. We covered the sensor and predictive approach in our article on smart cold forming with IoT sensors.
Aluminum wire picks up surface oxidation and contaminants quickly. Incoming wire should be clean, consistently annealed, and delivered with a known tensile strength and elongation. Storage should protect the wire from dust, moisture, and handling damage, because any surface defect becomes a galling starter.
Running aluminum on a former designed primarily for steel is possible, but it is not optimal. DongRui machines can be configured for aluminum with a combination of mechanical and control adjustments.
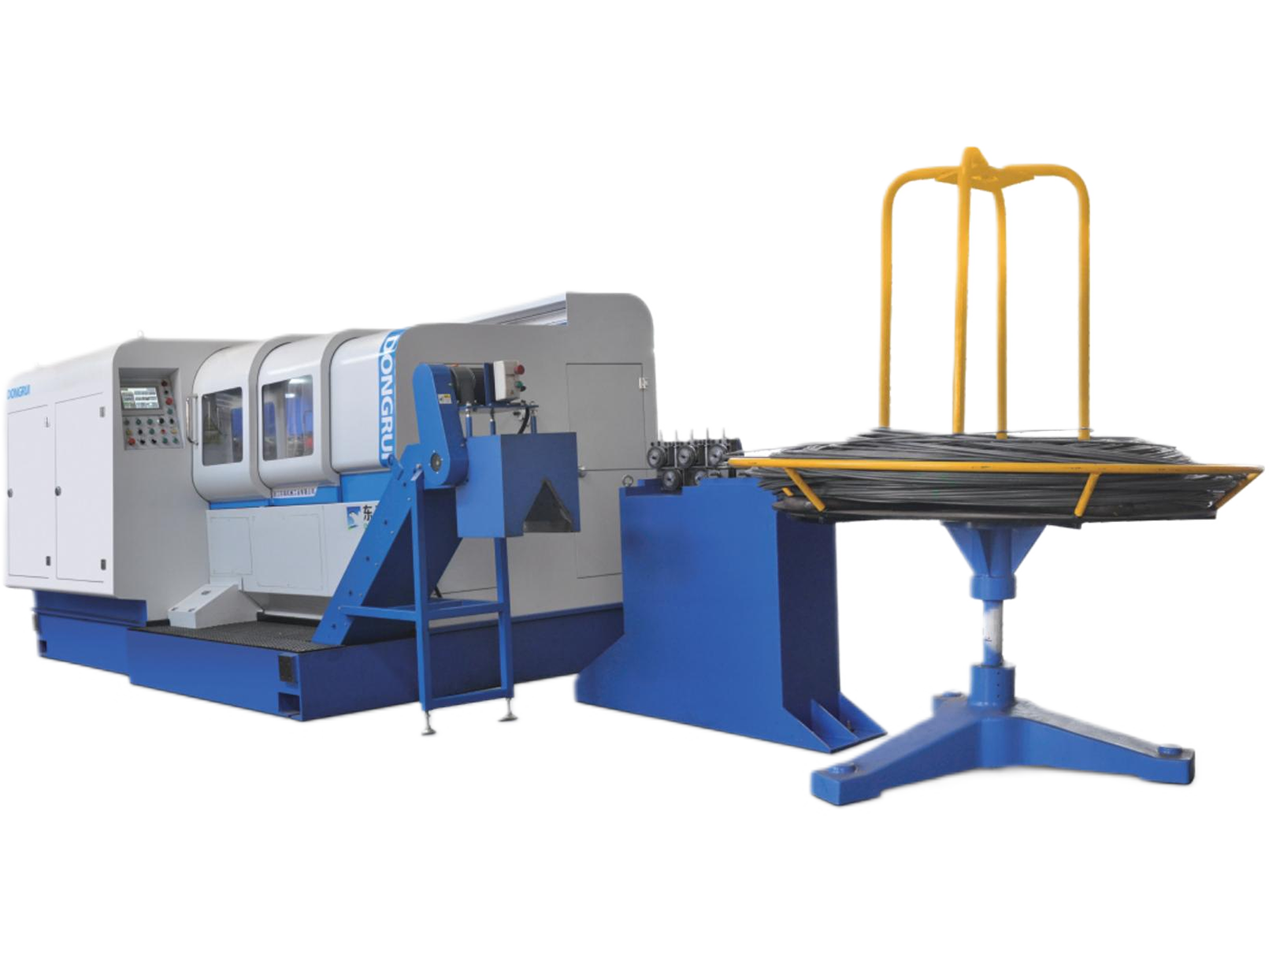
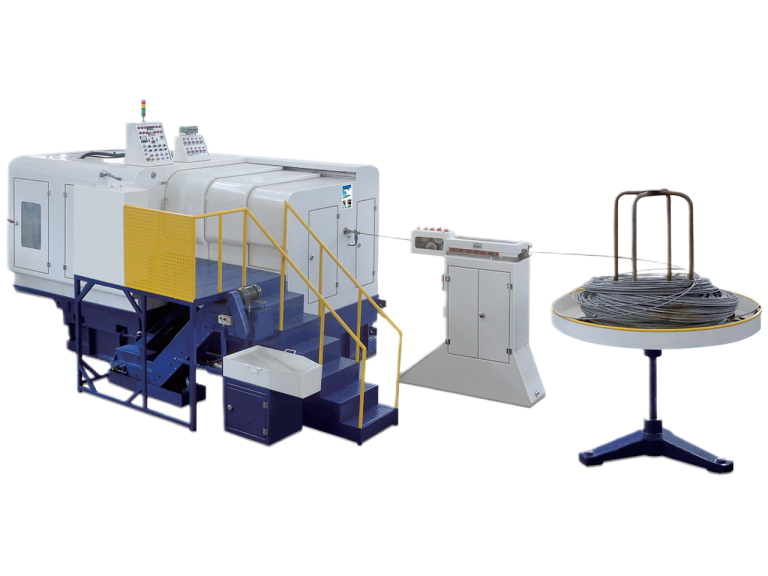
DongRui DBHP-8 high-speed automatic cold former — precision, stable transfer, and high output for small aluminum and steel fasteners.
The DBHP-8 automatic cold former machine with high precision is well suited to the small-diameter, high-volume fasteners common in electronics and lightweight automotive assemblies. Its high-speed output and stable transfer help maintain the surface quality that aluminum demands.
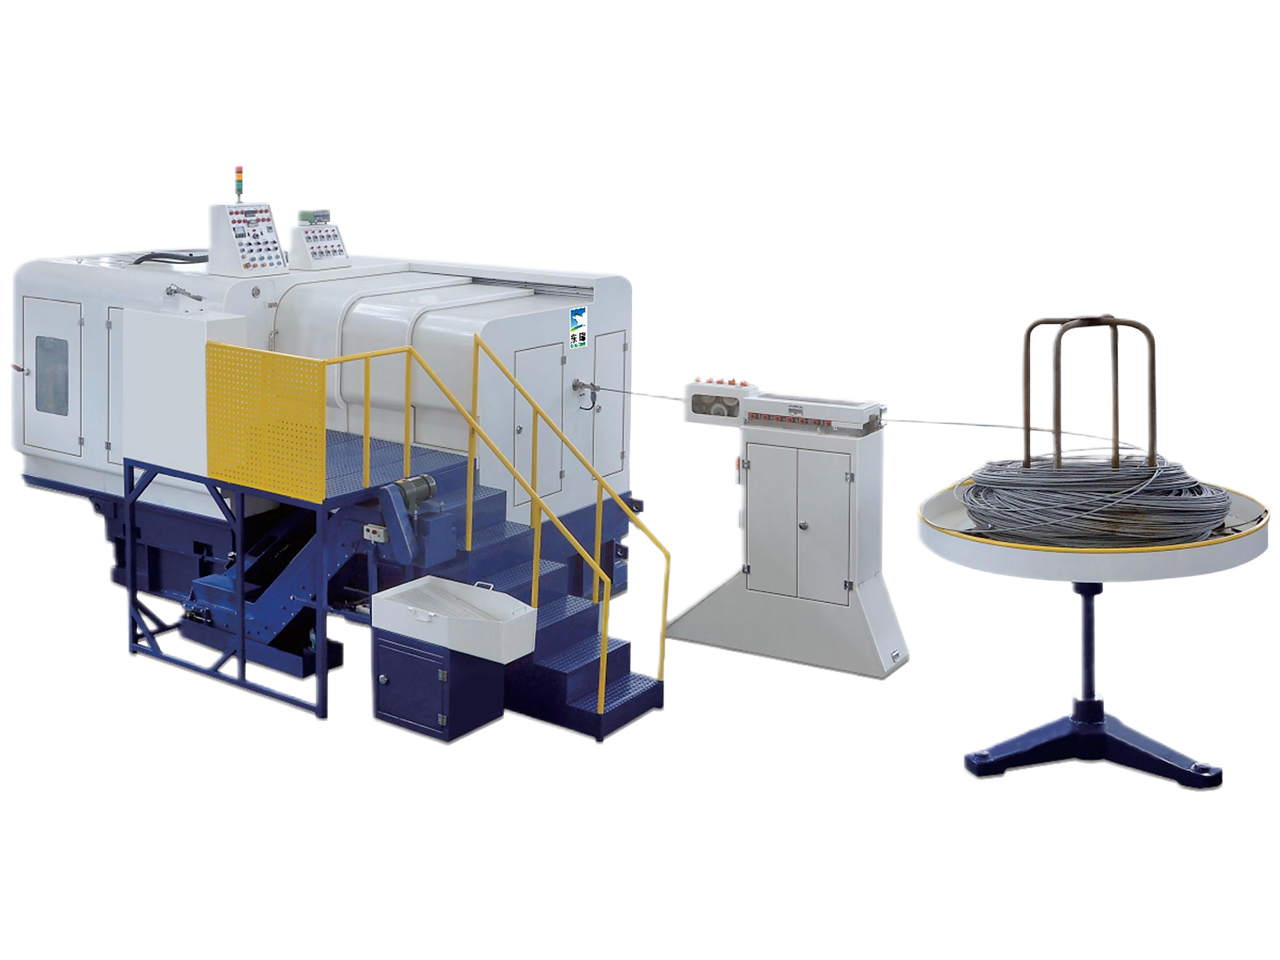
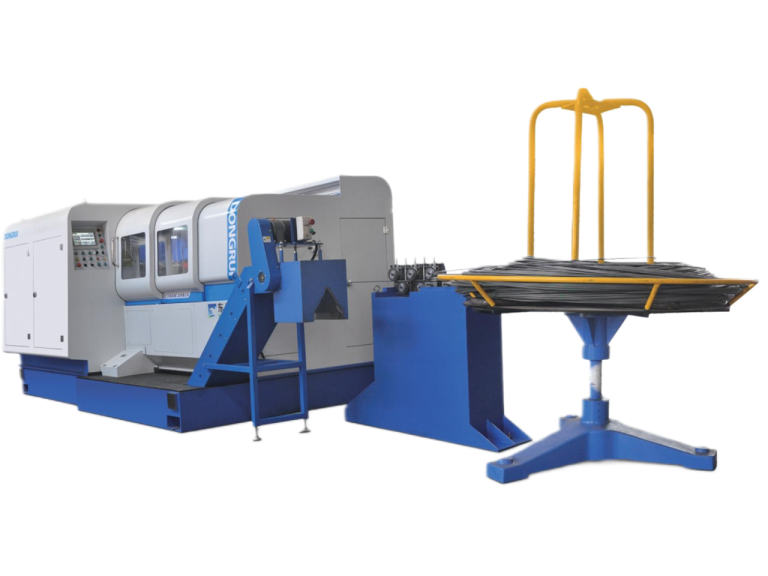
DongRui DBP-136LL multi-station cold heading machine — flexible station layout for aluminum prototypes and medium-volume production.
For parts that need more forming steps or frequent changeovers, the DBP-136LL multi-station cold heading machine offers the station count and adjustability to handle different aluminum alloys and head geometries on the same platform.
Entering the aluminum fastener market is not simply a material swap. Buyers in EV, electronics, and automotive have qualification requirements that go beyond dimensional checks. A practical expansion plan looks like this.
1xxx and 3xxx series are very soft and formable but low strength. 5xxx series offers better strength and corrosion resistance. 6xxx series, especially 6061 and 6063, balances strength, formability, and heat-treatability, and is widely accepted in automotive and structural applications. 7xxx is higher strength but less formable and usually reserved for aerospace.
Run forming trials to establish the safe upset ratio, springback compensation, and minimum calibration needed per station. Document the results by alloy, wire lot, and part number so the process can be repeated.
Many aluminum fasteners receive anodizing, passivation, or organic coatings after forming. The cold-headed surface must be free of scoring, folds, and lubricant residue for these finishes to adhere. Establish acceptance criteria with the customer early.
Electronics fasteners need high-speed, small-platform machines. Automotive structural fasteners need multi-station precision and higher tonnage. Choose a machine line that matches the largest part in the family without overspending on capacity that will not be used. Our guide to choosing the right cold heading machine provides a sizing framework.
| Expansion step | Key decision | Output |
|---|---|---|
| Alloy selection | Strength vs. formability trade-off | Approved material list per market |
| Formability trials | Safe upset ratio and springback | Process window for each part |
| Surface qualification | Finish adhesion and cosmetic limits | Customer-approved sample lot |
| Machine selection | Speed vs. station count vs. tonnage | Capital plan and quoting basis |
Scrap reduction is also part of the business case. Because aluminum wire is more expensive per kilogram than commodity steel in many regions, every gram saved matters even more. Our article on scrap reduction and circular economy in fastener plants shows how near-net shape cold forming turns material yield into profit.
Aluminum cold heading is moving from a specialty process to a standard capability. Lightweighting in automotive, the rapid growth of electric vehicles, and the relentless miniaturization of electronics are all pushing fastener demand toward materials that are lighter, non-magnetic, and corrosion-resistant. Aluminum meets those needs, but only if the forming process is set up with the right tooling, lubrication, and machine parameters.
The main obstacles — springback, galling, scoring, and work hardening — are all manageable with open die angles, anti-galling coatings, clean lubrication, controlled stroke speed, and multi-station deformation. Plants that master these controls gain access to high-margin markets where steel fasteners cannot compete.
DongRui offers the machine platforms to support that transition. From the high-speed precision of the DBHP-8 to the flexible multi-station layout of the DBP-136LL, DongRui formers can be tuned for aluminum with adjusted stroke, pressure, and transfer timing — giving fastener makers a practical path into the next generation of lightweight assemblies.
Explore the DongRui DBHP-8 High-Speed Cold Former
Related reading:
For general-purpose fasteners, 1100 and 3003 are very formable and economical, with good corrosion resistance but lower strength. For automotive and structural applications, 6061 and 6063 offer the best balance of strength, formability, and response to heat treatment. 5052 and 5056 are common where higher corrosion resistance or marine exposure is required. High-strength aerospace fasteners may use 7075, but its formability is lower and it usually requires more stations and tighter process control. The best grade depends on the required tensile strength, exposure environment, and whether post-forming heat treatment is allowed.
Heat-treatable grades such as 6061 and 7075 often benefit from a T6 temper to reach their full strength after forming. The forming operation itself introduces work hardening, which can add strength but also brittleness if over-done. A typical route is: solution heat treat after forming, quench, and then age to achieve the desired T6 properties. For non-heat-treatable grades such as 1100, 3003, and 5052, annealing is usually sufficient to restore ductility if the part was work-hardened excessively. Always validate the final temper with the customer’s torque-tension and corrosion requirements.
Aluminum can run at high speed, but the practical limit is usually lower than the machine’s maximum steel rating because surface temperature and lubricant film stability matter more. Many aluminum jobs run comfortably at 70–90% of the equivalent steel speed. Factors that reduce safe speed include large upset ratios, thin die coatings, marginal lubrication, and high ambient temperature. Starting at a moderate speed, monitoring part surface and forming load, and increasing speed only after the process is stable is the safest approach. In high-speed machines such as the DBHP-8, the transfer precision and rigid frame allow aluminum to run closer to the steel rating than older or less rigid formers.
Reading time: ~8 min | Categories: Cold Forging Technology, Equipment
Replace phosphate-and-soap wire pre-treatment with polymer coatings and eco lubricants.
Table of Contents Introduction What Is Cold Forging and Why

Titanium and Inconel 718 demand 2-2.5x the forming energy of
 Optimized by Seraphinite Accelerator